Executive Summary
Producing large-format polyethylene terephthalate (PET) containers ranging from 5L edible oil bottles to 20L (5-gallon) returnable water jugs introduces exponential mechanical, thermodynamic, and pneumatic engineering challenges compared to standard single-serve beverage lines. Heavy preform weights (120g to 750g), thick preform walls (4.5 mm to 8.5 mm), and massive projected cavity surface areas demand specialized stretch blow molding (SBM) machinery paired with high-rigidity mold tooling.
As a premier Chinese enterprise specializing in precision tooling, yushunmachine provides an authoritative technical guide detailing the core engineering requirements for 5L–20L container production. This white paper examines clamping tonnage mechanics, heavy-duty servo stretch rod kinematics, deep-penetration infrared heating profiles, and large-format blow molding machine mold construction required to achieve zero-flash, structurally rigid large containers.
1. Clamping Force Mechanics and Projected Area Calculations
In 5L–20L stretch blow molding, internal blowing pressures (typically 28 to 38 bar) act across a massive projected parting-line surface area. Insufficient clamping tonnage causes mold platen separation, resulting in ugly parting-line flash, uneven wall distribution, and premature tie-bar fatigue:
- Projected Area Force Dynamics: A single 20L water jug cavity presents a projected parting-line area exceeding 1,350 cm². At 35 bar internal blowing pressure, the outward separating force exceeds 47 metric tons per cavity.
- Multi-Point Toggle & Hydraulic Pressure Compensation: Large-container SBM machines utilize heavy-duty multi-point toggle linkages reinforced with hydraulic pressure-compensating cushions to lock mold halves rigidly throughout the high-pressure blowing phase.
- Sub-Micron Mold Locking Interfaces: High clamping tonnage must be matched by precision mold alignment hardware to prevent platen deflection and shear stress on guide pins.
2. Heavy-Duty Stretch Rod Kinematics and Axial Orientation
Stretching thick-walled large-format preforms over long axial strokes (up to 520 mm for 20L jugs) requires high-torque mechanical actuation and rigid guiding systems:
Kinematic Engineering Rule: Large-diameter stretch rods (22 mm to 30 mm) driven by closed-loop brushless servo motors are mandatory for 5L–20L containers. Precise velocity profiling prevents rod buckling upon initial gate contact and ensures uniform axial polymer distribution from shoulder to base.
A. Anti-Buckling Rod Geometry and Linear Guiding
Standard thin pneumatic stretch rods deflect under the high axial resistance of thick 650g preforms, causing off-center gate marks and severe wall thickness eccentricity. Heavy-duty machines employ hardened, large-diameter stainless steel rods supported by dual linear bearing blocks.
B. Contoured Tip Design for Thick Gate Zones
Custom multi-radius contoured stretch rod tips distribute mechanical stretching forces across a broader internal gate surface area, preventing localized pin-point punctures and optimizing base corner orientation.
3. Deep-Penetration Infrared Heating Profiles for Thick Preforms
Conditioning a 6.5 mm thick PET preform wall without scorching the exterior surface is one of the primary bottlenecks in large-container production:
- Extended Oven Dwell & Penetration Wavelengths: Thick preforms require longer heating tunnels with calibrated medium-to-short wave infrared emitters capable of penetrating deep into the polymer core.
- High-Velocity Surface Cooling Ventilation: Powerful forced-air cooling plenums strip excess heat from the outer preform skin while radiant heat conducts inward, maintaining an inner-to-outer wall temperature gradient within ≤ 3.0°C.
- Thermal Equilibration Zones: Dedicated non-heated equilibration zones between oven modules allow internal heat conduction to stabilize before the preform enters the blowing cavity.
4. Large-Format Mold Engineering: The yushunmachine Advantage
Even the highest-tonnage blow molding machine cannot produce consistent 5L–20L containers without specialized, structurally reinforced mold tooling engineered to manage high thermal masses and massive clamping loads.
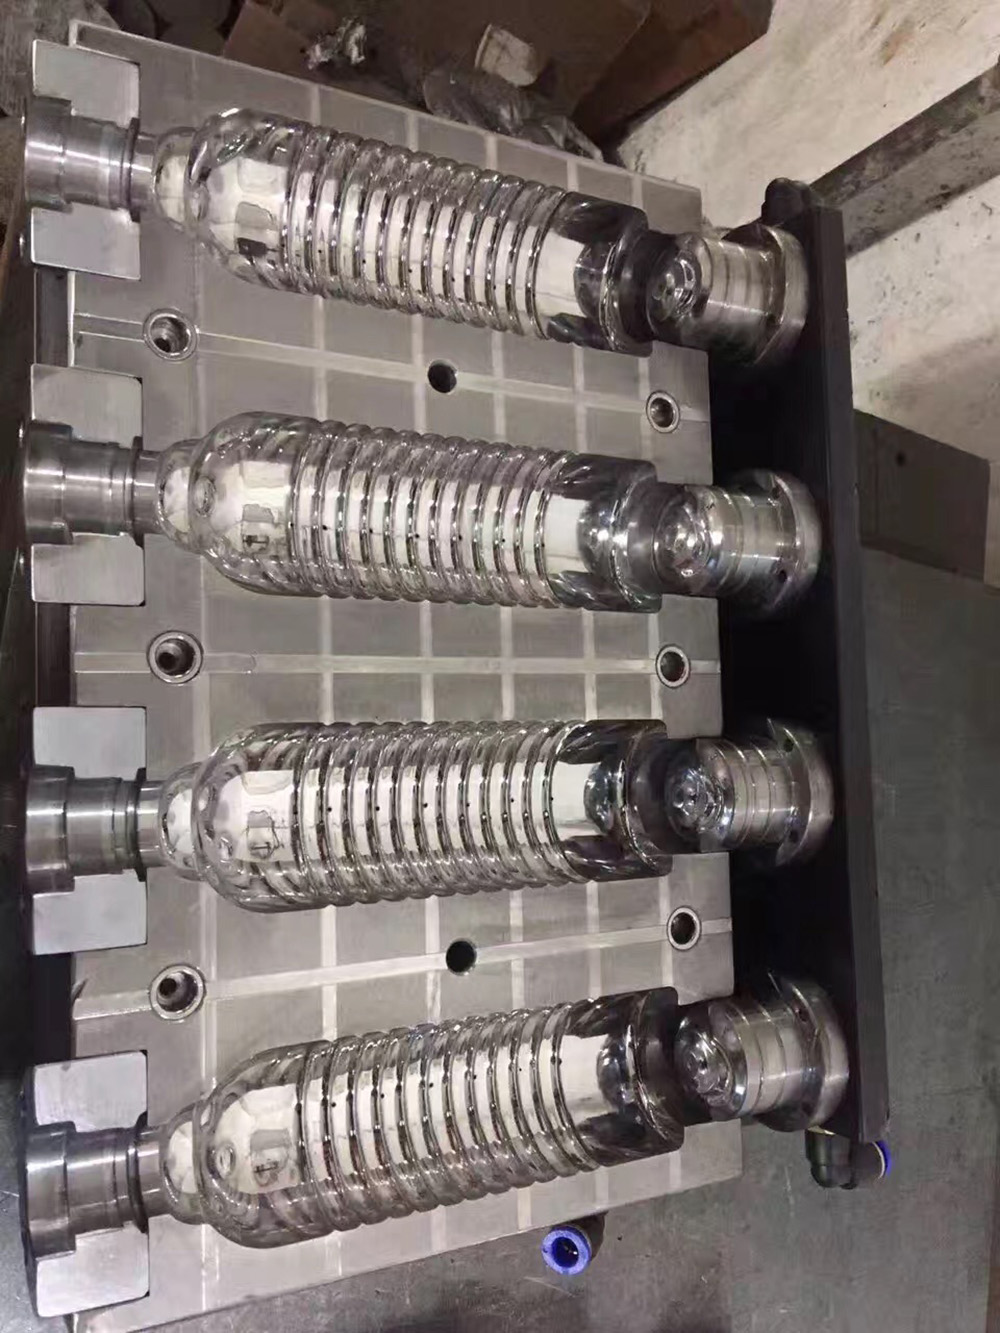
yushunmachine designs and manufactures custom large-format PET blowing molds, PET preform molds, and bottle blowing machine molds built for extreme durability:
- High-Tensile Metallurgy & Heavy-Wall Construction: Crafted from vacuum-quenched S136 stainless steel and forged 7075-T6 aircraft-grade aluminum with reinforced external rib structures to eliminate mold flexing under 50+ tons of clamping load.
- 3D Conformal Cooling & Independent Base Circuits: Thick 5L–20L container bases retain immense thermal energy. yushunmachine integrates high-flow 3D conformal cooling channels and dedicated base-insert water circuits to accelerate crystallization and prevent base roll-out.
- Quad-Stage Multi-Taper Self-Locking: Hardened precision taper locks distributed along the entire parting-line perimeter guarantee sub-micron concentricity (≤ 0.015 mm) across millions of production cycles.
- High-Capacity Micro-Venting Channels: Precision CNC-milled exhaust vents (≤ 0.025 mm) evacuate massive internal air volumes rapidly during inflation, preventing trapped air pockets and reducing high-pressure blowing requirements.
Engineering Specifications Matrix: 5L–10L vs. 15L–20L Container Production
The matrix below outlines key machine and mold tooling parameters across standard large-format container categories:
| Engineering Parameter | 5L – 10L Containers (Edible Oil / Water) | 15L – 20L Containers (5-Gallon Jugs) | Critical Tooling Requirement |
|---|---|---|---|
| Preform Weight & Wall Thickness | 120g – 240g (4.2 mm – 5.8 mm wall) | 450g – 750g (6.0 mm – 8.5 mm wall) | Balanced hot-runner preform molds |
| Required Clamping Force / Cavity | 18 – 28 Metric Tons | 45 – 65 Metric Tons | Quad-stage hardened taper locks |
| Stretch Rod Diameter & Drive | 20 mm – 22 mm Servo Driven | 26 mm – 30 mm High-Torque Servo | Contoured anti-puncture rod tip |
| Oven Heating & Equilibration | Multi-zone IR with moderate cooling | Extended tunnel + equilibration zones | Uniform ≤ 3°C through-wall gradient |
| Mold Cooling Architecture | High-flow sidewall & base channels | 3D Conformal Cooling + chiller loop | Rapid base crystallization control |
yushunmachine: Your Trusted Blow Molding Mold Solution Experts
Mastering 5L–20L PET container production requires seamless engineering alignment between machine clamping tonnage, servo stretch kinematics, deep thermal conditioning, and heavy-duty mold tooling. Compromising on mold metallurgy or cooling efficiency leads to parting-line flash, base instability, and high resin scrap rates.
yushunmachine is a premier Chinese enterprise delivering complete turnkey packaging tooling solutions. Specializing in large-format PET preform molds, PET blowing molds, and custom blow molding machine molds, yushunmachine equips global water, edible oil, and industrial chemical producers with reinforced alloys, 3D conformal cooling technology, and precision locking mechanics built for continuous heavy-duty output.
Launch or upgrade your 5L–20L container production lines with confidence. Contact yushunmachine today for specialized technical consultations and custom large-format mold proposals.